Drawn from archive notes on bag sewing routes and the factory's own line and inspection records.
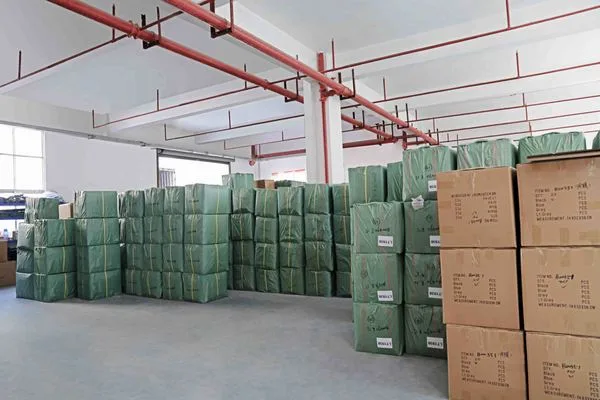
The cartons were stacked and strapped on the loading bay, and the forwarder's truck was already at the gate when the inspection report came back. A full batch of sewn bags, held at the dock over a seam that had passed the first piece check three weeks earlier. The container left empty that afternoon.
The buyer had done what most buyers do. She approved the sample, signed off the first piece, and trusted the line to keep repeating what it had proved on day one. What she had not asked was which kind of line was running her order, and what kind of failure that line was built to produce. The seam that stopped the shipment was not random. It was the exact failure her route was most likely to deliver, and it had been forming quietly since the first week.
The Carton That Never Left the Loading Bay

The defect itself was small. A run of stitches along one panel edge sat a few millimetres off the seam line, enough that the folded edge showed a raw lip when the bag was filled. On a single bag it would have been a second. Across the batch, it was the same deviation on piece after piece, repeating at a rhythm that matched the shift changes.
That repetition is what made the report fatal. An inspector who finds one bad seam in fifty bags writes a note. An inspector who finds the same bad seam in most of the cartons opens a different conversation, because the question stops being "how many are wrong" and becomes "when did the line start being wrong." The buyer could not answer that, and neither could the factory without digging back through its own records.
The truck left. The bags stayed. The launch date the buyer had built her marketing around moved, and the cost of the empty container sat on someone's ledger before a single replacement bag had been sewn.
Rewinding to the Station That Drifted
Going back through the production log, the seam did not fail all at once. It drifted. The machine that set that panel edge had been calibrated at the start of the run, checked against the first piece, and then left to run. Somewhere in the middle of the batch, a guide moved slightly, or a needle wore, or the tension crept. Nobody caught it because nobody was looking at the middle of the batch.
This is the signature of an automated line. It produces highly consistent seams, and that consistency is exactly what makes a batch failure possible. When the station is right, every bag is right. When the station drifts out of calibration, every bag after the drift carries the same error, and the volume of identical defects is what turns a minor tolerance issue into a rejected shipment.
The first piece check had done its job. It confirmed the line was set correctly on day one. What it could not do was confirm the line was still set correctly on day fifteen. The check was a snapshot, and the failure lived in the gap between snapshots.
Why the Same Seam Fails Twice in Two Different Ways

Put the same seam on a manual bench and the failure looks nothing like this. A skilled sewer working the panel edge produces variable seams, because hands are not machines. The stitch line wanders a little, the tension changes with the operator's pace, and occasionally a stitch is skipped entirely. Those defects are scattered through the batch rather than concentrated in a block.
That scatter changes the entire inspection logic. A scattered defect pattern is what AQL end-of-line sampling is built to catch. Pull a random sample, count the defects, compare against the limit, and the statistics tell you whether the batch is acceptable. The defects are distributed, so the sample represents the whole.
A batch-consistent defect breaks that logic. If the error started at carton forty and continued to the end, a random sample of twenty bags might miss it entirely, or might hit it hard, depending on where the draw falls. The sample stops being a fair proxy for the batch. That is why the buyer's end-of-line inspection passed a shipment that a first-piece-and-inline check would have stopped at the station.
Neither route is safer. They fail in different shapes, and the shape decides which check catches them.
The Evidence in the First Piece and the Last Piece
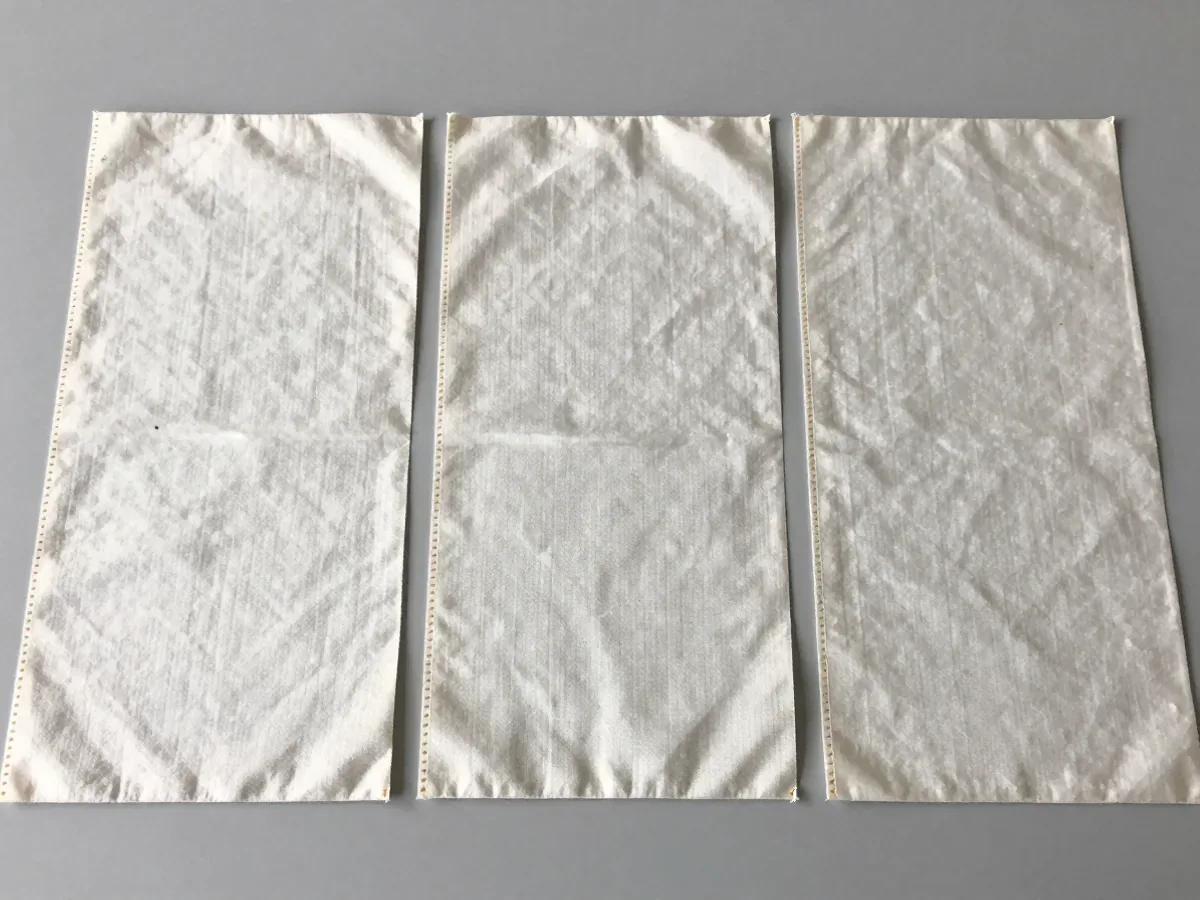
The most useful thing the buyer could have done costs almost nothing. Keep the first piece, keep a piece from the middle of the run, and keep the last piece off the line. Lay them side by side on a table and look at the seam.
On an automated line, three pieces from three points in the run tell you whether the station held its calibration. If the first piece is clean and the last piece shows the drift, the failure is a calibration story, and the fix is a schedule of in-line checks rather than a single gate at the start. On a manual line, the same three pieces will show normal variation, and the question shifts to whether the scatter is inside the AQL limit.
The factory in this case had the evidence. The pieces existed. Nobody had asked for them to be compared, because the inspection plan was written around the sample, not around the route. A first piece check and an end-of-line AQL are both good tools. They answer different questions, and the route decides which question matters.
What the Repair Cost Actually Bought
The rework on that batch was not just sewing time. It was unpicking, re-cutting panels where the seam had weakened the edge, re-sewing, and re-inspecting. The cartons had to be reopened, the bags re-counted, and the shipment re-booked. The visible cost was the labour. The hidden cost was the two weeks of production capacity that went into fixing bags that had already been counted as finished.
That capacity came out of the next order. A factory running eight bag series on the same lines, stock and custom together, cannot absorb a rework block without pushing something else. The buyer's replacement bags arrived, but they arrived behind a queue that her own rework had created.
The repair also bought a lesson the buyer did not want to pay for twice. The next order carried a different inspection plan. It specified a first piece check, an in-line check at the middle of the run, and a final inspection before packing, with the three reference pieces kept and photographed at each stage. The plan cost a few hours of inspector time. The rework had cost two weeks.
Where the Two Routes Cross on Order Size
The choice between the two routes is not a quality choice. It is a volume and complexity choice, and it sits on a curve that crosses somewhere between two thousand and ten thousand units per SKU, depending on how many seam paths the bag carries and what local labour costs.
Below that crossing, manual sewing usually undercuts automated production because there is no setup cost to amortize. A manual team can start an order of five hundred units without a setup charge hanging over the unit price, switch between SKUs in minutes, and handle curved seams, padded straps, and zippered compartments that an automated line cannot manage without retooling. For most custom bag orders, that flexibility is why the bench still wins.
Above the crossing, the automated line's throughput and consistency start to pay, and the advantage widens as volume grows. Long runs with simple seam structures, two or three seam paths and little variation, are where automation earns its place. The buyer's order in this case sat in the middle, large enough to justify the automated route and varied enough that the route's failure mode was never planned for.
Sewn bags need no tooling, so a new pattern is proved on one sample round. That low barrier is why so many custom orders move between routes without anyone rethinking the inspection plan. The route changed. The checks did not.
A Buyer Checklist That Follows the Defect, Not the Label
The label on the factory says automated or manual. The label does not tell you how the order will fail. The defect shape does, and the checklist should follow the shape.
- Ask which route will run the order, and ask it in writing on the PO rather than in a call.
- For an automated route, require a first piece check plus scheduled in-line checks through the run, with the station calibration logged at each check.
- For a manual route, require AQL end-of-line sampling sized to the batch, and confirm the sampling plan matches the scatter you expect.
- Keep three reference pieces from the run, first, middle, and last, photographed at the seam that carries the most load.
- Confirm that pull, seam strength, and bar tack are tested on every batch, not only on the sample.
- If the factory switches routes mid-order, rewrite the inspection plan before the first carton is sealed, because the old plan was built for a different failure.
- Put the final inspection and packing stage on the schedule with a named sign-off, so the last check is a gate rather than a formality.
None of these steps require a new supplier or a bigger budget. They require the buyer to know which failure her route produces and to place the check where that failure would show. The cartons on the loading bay failed because the plan was built around the sample, and the sample was never the part of the order that went wrong.
FAQ
Do automated sewing lines produce fewer defects than manual lines?
They produce more consistent seams, which is not the same thing. An automated line fails in batches when a station drifts out of calibration, and a batch failure can be larger than the scattered defects a manual line produces. Manual sewing shows scattered defects that AQL sampling is designed to catch.
At what order size does automated sewing start to pay off?
The cost curves typically cross between two thousand and ten thousand units per SKU, depending on seam complexity and local labour rates. The advantage widens as volume grows, and below the crossing manual sewing usually undercuts automated production.
Why do most custom bag orders still run on manual sewing?
Manual teams switch between SKUs in minutes, handle curved seams, padded straps, and zippered compartments without retooling, and start a five hundred unit order without a setup cost to amortize. Sewn bags need no tooling, so a new pattern is proved on one sample round.
Should the inspection plan change if the factory switches routes mid-order?
Yes. A batch-consistent defect from an automated station and a scattered defect from a manual bench are caught by different checks. If the route changes, the first piece and in-line checks or the AQL sampling plan has to be rewritten before the run continues.